
How to choose a custom portable tableware manufacturer
Choose a custom portable tableware manufacturer by defining the complete set first, then checking the responsible production route, tooling or existing-component options, multi-material coordination, quality controls and one accountable sample-to-packout process. Compare suppliers against the same specification and evidence list. A polished catalog, a generic certificate or an illustrative factory image cannot establish capability for your particular SKU.
Portable tableware is a system rather than one molded object. A lunch box may have a separate lid and seal; the cutlery may be metal; the case may be textile; and the final sales unit may need inserts, printed packaging and market-specific paperwork. A buyer should evaluate whether one supplier can define, coordinate and control that system, while identifying which processes happen at its own facility and which use qualified partner routes.
This guide is a decision framework, not an independent audit of Naike or any other company. Naike’s published About page describes its B2B coordination of portable dining sets, manufacturing routes, carry goods, packaging and quality review. The responsible facility, capacity and evidence are stated there as project-specific matters. Do not infer unpublished machine counts, output figures, certificates or customer results.
Start the Custom Portable Tableware Manufacturer Brief
Specify the people who will use the set, the eating occasion, carrying route, cleaning method, sales channel and target market. List every component in the proposed sales unit: food container, lid, utensils, cup, pouch or case, insert and retail pack. Describe how the pieces should nest, how the case opens, and how the finished pack will be stored and shipped.
Separate requirements from preferences. A maximum packed envelope may be mandatory; one color family may be negotiable. Leak resistance, microwave use, dishwasher use, food-contact suitability and service life are claims that require conditions and SKU-matched validation, not assumptions based on a material name. State the intended food, temperature, contact time, cleaning route and destination before asking for declarations or testing.
| Brief field | Buyer input | Supplier response |
|---|---|---|
| Complete set | Component count and use case | Proposed BOM and exceptions |
| Carry and pack | Maximum envelope and access needs | Packing layout and sample route |
| Customization | Color, logo and structure priorities | Existing parts versus new tooling |
| Target market | Destination and intended contact | Applicable evidence plan |
| Commercial | Quantity, timing and delivery terms | Itemized, assumption-led quote |
A consistent RFQ allows a fair comparison. If one quotation includes the carry case, testing and printed carton while another covers only molded pieces, the prices are not comparable. Ask suppliers to mark exclusions, open technical decisions and ownership of each process, not merely confirm a total price.
Compare Factory, Trading and Coordinated Supply Models
“Manufacturer” can describe several arrangements. A direct molding facility may control its own molding and trial process but source metal cutlery and textile bags. A trading business may connect several producers without owning production. A coordinated network may combine a core manufacturing route with identified specialist partners and one project manager. None is automatically superior for every set; disclosure and control are more useful than a simple label.
| Model | Potential strength | Question to test |
|---|---|---|
| Direct factory | Clear process owner for selected components | Which parts and steps are made here? |
| Trading partner | Broad sourcing flexibility | Who approves samples and handles nonconformity? |
| Coordinated network | Multi-material set management | Who owns the BOM, interfaces and final packout? |
Request a process map. It should identify molding, metal forming or finishing, textile cutting and sewing, decoration, assembly, inspection and packing as applicable. For each step, ask for the responsible entity, transfer point, control document and escalation owner. If a process is outsourced, the final supplier still needs a clear method for revision control and corrective action.
Test Engineering, Existing Components and Tooling Choices
Before commissioning a mold, ask whether an existing component platform can meet the brief. Review actual samples, drawings and the limits of color, lid geometry, wall thickness, nesting and decoration. A new tool can create differentiation but also adds design-for-manufacture review, prototype revisions, acceptance criteria, ownership terms, maintenance and schedule risk.
Ask a candidate supplier to explain the development stages from brief to drawing, sample, fit test and approval. Require an identifiable revision for the box, lid, case insert and retail packaging. Interfaces deserve special attention: the lid must fit the approved box; a fork should not puncture its sleeve; and the filled case must close without distortion. A component-level approval alone is not a set-level approval.
For a proposed custom tool, compare assumptions about design files, tolerance, mold ownership, trial parts, revision count, approval samples and spare-part compatibility. Do not infer tooling availability from a picture of a mold room. Request a numbered tool and relevant trial sample if an existing-tooling claim matters to the buying decision.
Ask for Quality Controls at Each Handoff
Quality assurance starts with an agreed specification. Ask how incoming resin or sourced components are identified, how a first article is approved, what is checked during production, and how final set counts, lid fit, colors, decoration and case packing are verified. The answer should identify records and responsible roles, not just say “100% quality control.”
For food-contact components, request evidence that matches the finished SKU, selected material, color and destination market. A report for another resin, older construction or different item may be useful background but does not automatically support a new claim. The inspection plan should specify which characteristics are critical, how defects are recorded and what happens to nonconforming stock.
Distinguish three kinds of material: a conceptual image explains an intended workflow; a supplier-provided photograph may show a facility but still needs provenance; and a project record ties a named SKU, date, process and result to a claim. The generated images in this guide are illustrations only. They do not establish Naike’s equipment, capacity, inspection results or the origin of any physical sample.
Map Multi-Material Responsibility and Packout
Portable sets often combine molded plastic, metal, textile and paper. Require a single bill of materials with part numbers, finish and color references, packing sequence and replacement rules. Identify who checks supplier changes before they reach the final assembly line. A different zipper, lid revision or textile thickness can affect the finished case even when each component passes its own incoming check.
Ask the supplier to demonstrate before-packing, packed and carrying states. The two-person portable tableware sample set concept illustrates why buyers should see components laid out, placed into a partitioned case and closed as a complete unit. It is a proposed configuration, not a confirmed production SKU; packed dimensions, weight, material declarations and performance remain to be established with a physical sample.
Review carton count, retail packaging, barcode or label requirements, shipping protection and replacement components together. The manufacturing network and quality coordination pages describe Naike’s published service approach; an RFQ should still identify the responsible facility and evidence for the exact project.
Approve a Complete Physical Sample Before Production
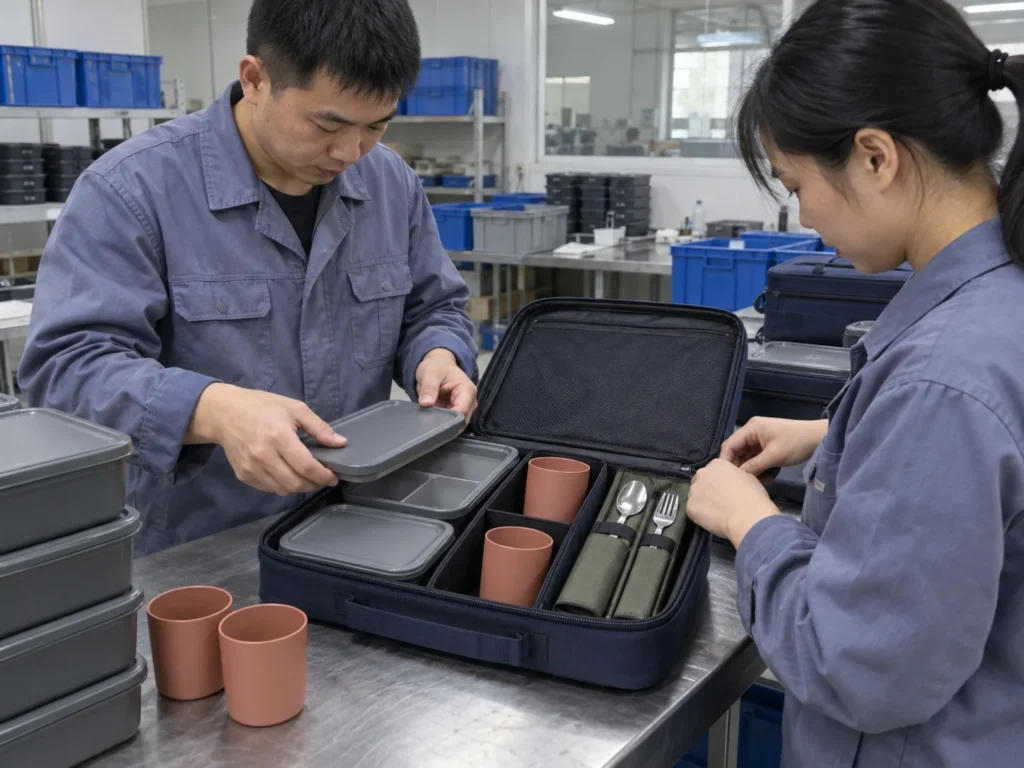
Ask for a sample that represents the proposed bill of materials and packing instructions. Check each part against the drawing, then assemble and repack it using the intended sequence. Measure the closed case, weigh the complete set, try the handle and zipper, inspect movement during handling and check whether components remain accessible. Record failures and revisions before accepting a signed sample.
Do not approve a concept render as a production-ready SKU. A render helps discuss arrangement; a physical sample tests fit, tactile finish and assembly. A test document should name the item and conditions it actually covers. When design or materials change, decide which checks need repeating. MOQ and lead time should follow the approved route rather than an unqualified universal promise.
Use One Manufacturer Selection Scorecard
Identity and route
Evidence to request: Responsible facility and process map.
Risk if unclear: Unclear accountability.
Engineering
Evidence to request: Drawings, revisions and sample stages.
Risk if unclear: Fit changes after approval.
Tooling
Evidence to request: Existing tool sample or new-tool terms.
Risk if unclear: Ownership and schedule dispute.
Quality
Evidence to request: SKU-level criteria and records.
Risk if unclear: Unsupported performance claim.
Coordination
Evidence to request: BOM, partner roles and packout.
Risk if unclear: Incomplete sales unit.
Commercial
Evidence to request: Quote assumptions and exclusions.
Risk if unclear: Non-comparable prices.
Score what can be demonstrated, record what remains unconfirmed and use the same weighting for every candidate. A lower unit price may be attractive if development and evidence are controlled; a higher price may be justified by testing, case engineering or clearer responsibility. Neither conclusion follows from a hero image or a general claim of factory experience.
For Naike, use the information on its public About page as a starting description, then ask the team to confirm the route, sample, facility and documents for your brief. Do not assume every component uses the same facility. The best short list is one that can answer the buyer’s exact configuration and show how uncertainties will be resolved before production.
Is a factory website enough to verify a manufacturer?
No. Use the website to understand stated scope, then request the responsible facility, production route, sample, project-specific evidence and a clear list of exceptions.
Must every component be produced under one roof?
No. What matters is a disclosed responsibility map, controlled bill of materials, compatible components, sample approval and accountable final packout.
Can an AI-generated factory image prove equipment or capacity?
No. A conceptual image illustrates a workflow only. Ask for identifiable, permission-cleared factory evidence and records when a capability claim needs verification.
Which information should the first RFQ include?
Share users, set configuration, materials, target market, quantities, branding, packaging, desired schedule and any limits on packed size or weight.
When should MOQ and lead time be compared?
Compare them after each supplier quotes the same approved configuration, sample route, tooling, testing and packaging assumptions.
Send a Brief That Can Be Evaluated
Share the intended users, component list, carry format, destination market, quantities, branding, packaging, target schedule and any must-have packed envelope. Request a route map, sample plan, exceptions and itemized quotation. Then compare the complete proposed sales unit, not just a lunch box price.